
The Hidden Cost of Conveyor Downtime and How to Prevent It

Vijay Baid
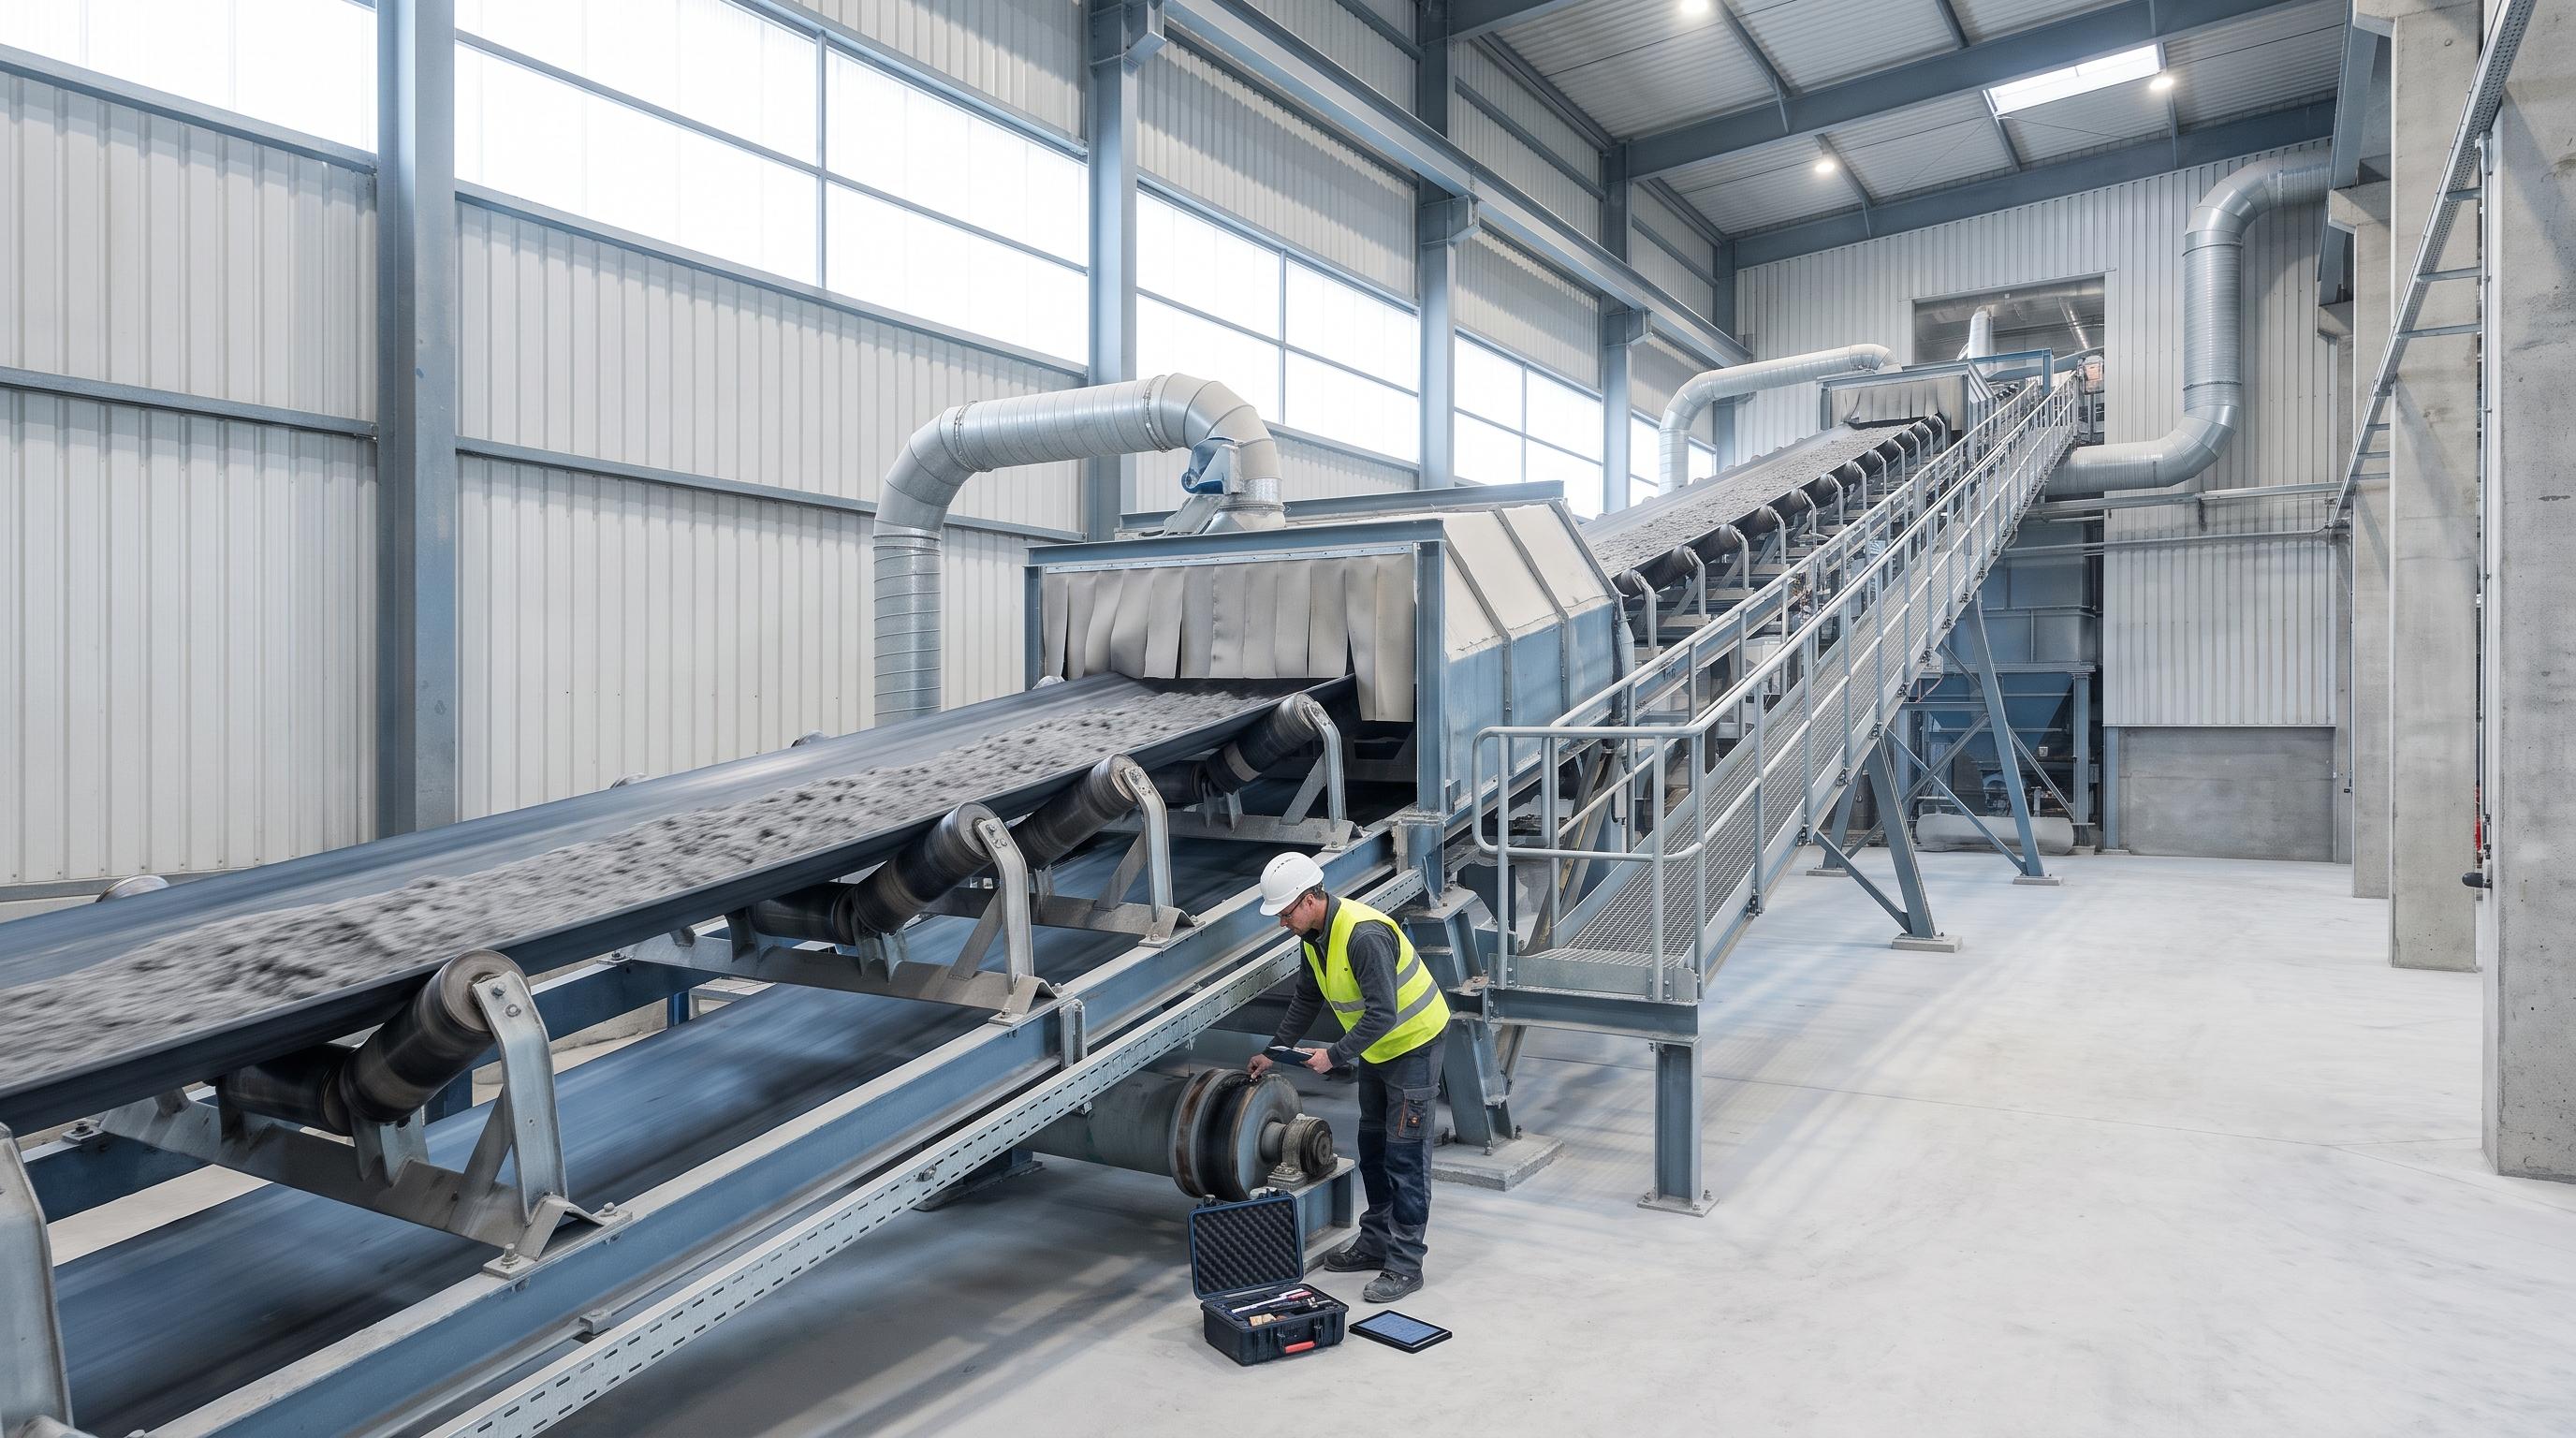
Downtime is rarely just a repair bill. In plant reviews, the real loss usually comes from stalled output, carryback, belt damage, and unplanned cleanup. Most failures start with small signs that were visible earlier, such as belt drift, dust leakage, or early idler distress. A stronger plan starts with correct idler selection, stable belt tracking, and tighter sealing at transfer points.
In most plants, a conveyor failure does not stay a conveyor problem for long. We often see one stoppage affect feeders, hoppers, truck movement, and downstream equipment within minutes. The failed part may be cheap. The production loss around it is not.
Many teams still count only labour and spare parts when they think about downtime. On site, that is rarely the full picture. Lost output, cleanup time, secondary damage, and safety exposure usually add up faster than the repair bill. That is why shutdown reviews should look beyond maintenance cost and focus on what the stoppage did to the full line.
The Financial Ripple Effect of a Line Failure
When a conveyor handling raw materials drops offline unexpectedly, the financial consequences mount minute by minute.
1. Direct vs. Indirect Financial Realities
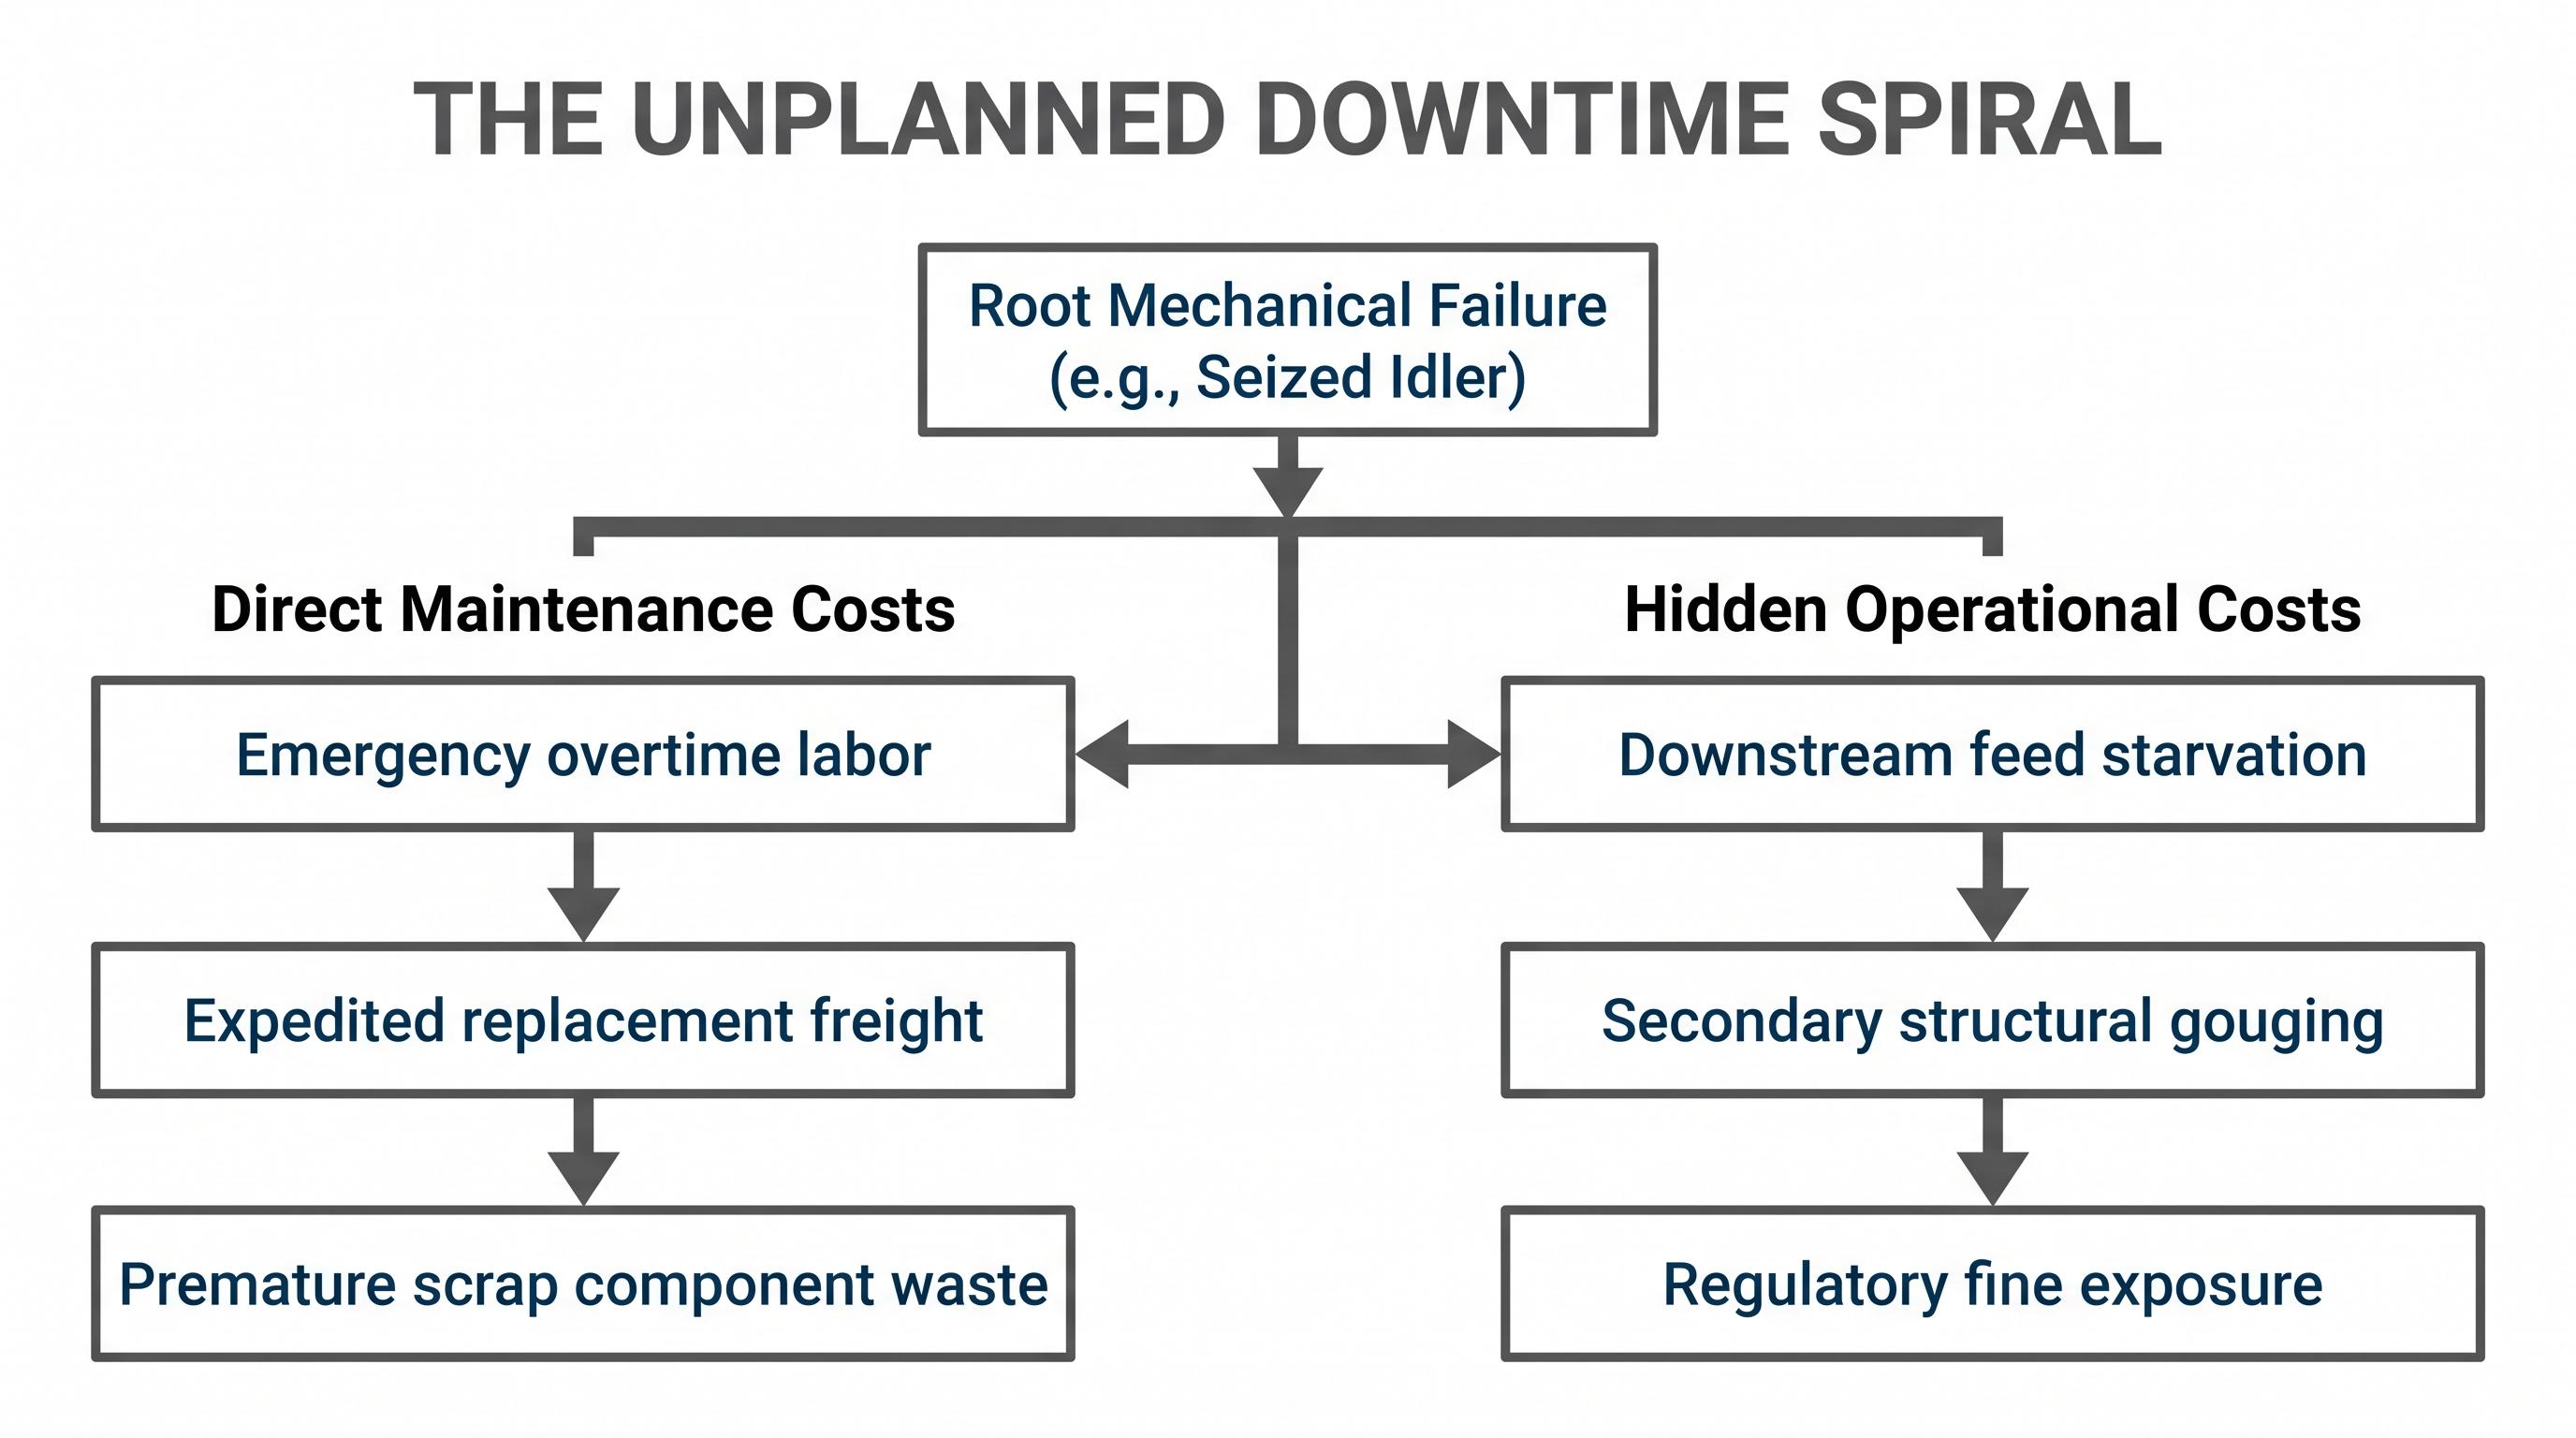
Direct costs are easy to see. Overtime labour, urgent parts, and crane support show up fast. The harder part is the loss around them. In shutdown reviews, we often find the bigger hit comes from missed throughput, unstable kiln feed, or extra handling to keep material moving. That is why short stoppages can become expensive even when the repair is small.
2. Secondary Mechanical Damage
A mechanical failure rarely stays isolated. When one weak component breaks, it often starts a chain of damage across the system. A common example is a roller bearing that seizes after dust gets inside. The roller stops turning and becomes a fixed brake surface. The moving belt then drags across the locked shell. Over time, friction cuts the metal into sharp edges. If nobody stops the line, those edges can slice the belt and turn a simple roller change into a full belt replacement.
Technical Comparison: Maintenance Management Strategies
To stop unexpected shutdowns, plants must move away from reactive "run-to-failure" habits. The matrix below compares the three main maintenance strategies used in modern material handling systems:
Performance Metric | Reactive (Run-to-Failure) | Preventive (Time-Based) | Proactive (Root-Cause Prevention) |
Operational Philosophy | Fix it only when it breaks | Replace parts on a fixed schedule | Eliminate failures through engineering |
Unplanned Outage Risk | Extremely High | Moderate (Parts can fail early) | Low |
Component Service Life | Wasted (Parts fail prematurely) | Trimmed (Good parts discarded early) | Maximized (Components run to full potential) |
Initial Capital Expense | Zero | Low to Moderate | Moderate to High |
Long-Term Plant OpEx | Volatile and High | Predictable but Inefficient | Lowest Total Cost of Ownership |
Best Applied To | Non-critical, isolated lines | Standard lubrication schedules | High-capacity primary feed systems |
Stop costly conveyor failures before they disrupt production. Let our engineers evaluate your material handling system for improved performance and lower maintenance.
The Leading Root Causes of Convey or Failures
Most unexpected conveyor shutdowns follow a pattern. In site audits, the same three issues show up again and again. The warning signs are usually visible early, but they get treated as minor housekeeping problems until the line is forced down.
1. Incorrect CEMA Component Selection
Undersized components often fail early. Light-duty rollers on high-tonnage lines can bend under load. That bend throws the internal bearings out of line. The bearings then run hot, lose lubrication, and seize before reaching their expected service life.
Shaft Deflection => Bearing Misalignment => Lubricant Loss => Idler Seizure
Correct shaft sizing and load rating should be checked against the official CEMA (Conveyor Equipment Manufacturers Association) reference during design, not after repeated failures in service. In field reviews, we often find light-duty rollers installed on duty conditions they were never meant to carry. On high-capacity lines, heavy-walled CEMA D or E rollers with multi-stage labyrinth seals usually hold up far better against dust, moisture, and shock loading.
2. Neglected Belt Tracking Errors
A mistracking belt almost always leaves signs before a major failure. On site, we usually spot edge rubbing, fine spillage near the structure, and uneven wear around the loading zone. If that drift is left alone, the belt edge opens up, moisture gets in, and nearby equipment starts taking extra wear. That includes Diverter Valves and chute liners.
3. Inadequate Transfer Point Sealing
Poor sealing at the transfer point creates more than a dust problem. In plant inspections, this is often where we see carryback, skirt damage, dirty walkways, and fast wear on nearby rotating parts. When heavy material hits the belt without proper support, the impact zone turns into a constant maintenance point. That wear can spread to Flow Control Gates and Screw Conveyors as well.
Download engineering data sheets with dimensions, load ratings, and seal configurations for accurate project planning.
Final Takeaway
Reducing conveyor downtime starts with matching each component to the duty it must handle. In practical terms, that means using correctly rated idlers on main carrying runs, protecting loading zones with proper impact support, and correcting belt tracking before edge damage becomes structural damage. Small engineering corrections made early are usually far cheaper than long shutdown repairs.
When the conveyor runs steadily, the rest of the plant feels the benefit. Material moves cleanly, downstream equipment stays better protected, and teams spend less time firefighting repeated faults. In our experience, stable conveying improves reliability across connected systems such as Dampers, packhouse circuits, and silo feed lines.
Frequently Asked Questions (FAQ)
To find the true cost of downtime, use this engineering formula:
Total Hourly Cost = Lost Production Value + Emergency Maintenance Labor+ Expedited Replacement Costs +Secondary Damage Depreciation
In high-volume operations, the value of lost production throughput usually dwarfs all other direct repair costs combined.
Standard steel rollers cannot absorb heavy impact forces. When large chunks of material fall from high chutes, the impact bends the internal shafts and shatters the rigid bearings. In heavy impact zones, you should always replace standard steel rollers with specialized rubber-ring impact idlers or structural impact cradles.
Yes. Escaping dust acts as a highly abrasive grinding paste when it mixes with bearing grease. Once this dust gets past basic lip seals, it locks up the rolling components, creating frozen surfaces that quickly cut into your expensive conveyor belts.
Watch for early indicators like slight belt tracking shifts, small piles of spilled material under transfer points, squealing bearings, and flat spots on rollers. Catching these signs early during regular inspections lets you plan minor repairs during scheduled maintenance windows before they turn into major emergency shutdowns.
Training idlers use a central pivoting mechanism. When the conveyor belt drifts off-center, the edge of the belt contacts a guide roller, which pivots the entire idler frame slightly. This angled position guides the moving belt back to the center of the structure without causing edge wear.